The cheapest cutting tool on the quote is rarely the cheapest tool in your spindle. After six years of tracking every insert, end mill, and tool holder that crossed our receiving dock, I can tell you that sticker price explains maybe 40% of what you actually pay per machined part. The other 60% hides in cycle time, tool changes, scrap rates, and the afternoon your operator spends re-zeroing a tool that wasn't ground to spec.
I'm a procurement manager at a 180-person machining shop. I've managed our tooling budget—$340,000 annually—for six years, negotiated with more than 40 vendors, and logged every order in our cost tracking system. In Q1 2024, I ran the numbers on $2.1 million in cumulative tooling spend. The pattern was ugly and consistent: the lowest-quote vendor won the purchase order 70% of the time. They won the cost-per-part comparison almost never.
Why the Quote Sheet Lies to You
Here's what most people don't realize about cutting tool pricing: the number on the quote is deliberately isolated from the variables that actually drive your cost. A seco tools cutting tools distributor will quote you $18 for an indexable insert. A budget importer will quote $11 for the "same" ISO classification. The $7 gap looks like a no-brainer on a purchase requisition.
Then you run the insert.
On our Okuma lathes, the $11 insert lasted 40% fewer passes on 4140 steel. That's not a knock on budget tooling as a category—it's a fact of life when hardmetal grade consistency isn't there. We changed inserts more often. Each change costs about 4 minutes of spindle downtime plus operator attention. Across a 500-piece run, that added up to 14 hours of lost production. At our shop rate, that's $1,260 in machine time. On a purchase order where we saved $140.
"The $7 difference per insert turned into a $1,120 net loss per run. Not because the cheap tool was 'bad.' Because I was comparing the wrong numbers."
The Causation Runs Backward
People think premium cutting tool brands charge more because they can. Actually, it's the other way around. Vendors who deliver consistent tool life, tight tolerance on the carbide substrate, and predictable wear patterns can charge more—because their product creates measurable value in the spindle. The causation runs from performance to price, not price to performance.
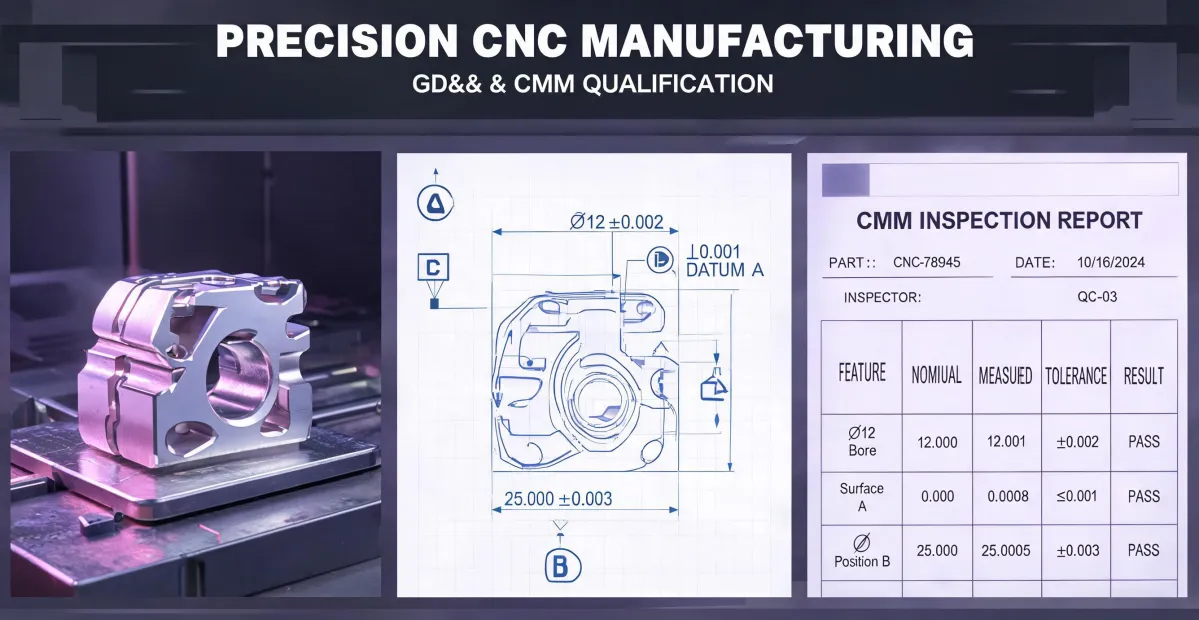
This sounds obvious when you write it down. It wasn't obvious when I was staring at three quotes for seco cutting tools, trying to justify a 35% premium to my operations manager. What changed my mind was a TCO spreadsheet I built after getting burned twice on hidden costs. I started tracking cost-per-part instead of cost-per-insert. The premium tools won on 7 of our 10 highest-volume jobs. On the other 3, the mid-tier option was actually better—which brings me to a point most procurement guides skip.
Where the Premium Argument Breaks Down
Everything I'd read about tooling said premium always pays off. In practice, that's only true when you're running high-volume, tight-tolerance work where tool failure means scrap. For our low-volume prototyping jobs—maybe 20 pieces, loose tolerances, forgiving material—the mid-tier import tool was fine. Not great. Serviceable. The premium insert lasted longer, but we didn't need it to. We needed it to cut 20 parts and get out of the way.
So we split our purchasing policy. High-volume production: seco-tools and comparable premium lines, no exceptions. Prototype and short-run: mid-tier, with a documented quality check on the first part. That policy cut our tooling spend by 12% without touching our scrap rate.
The Press Brake Problem
You might wonder why a procurement manager for cutting tools is talking about hydraulic servo press brakes. Here's why: in our shop, the press brake and the machining center are both cost centers, and the purchasing logic that works for one doesn't transfer to the other. A hydraulic servo press brake has a completely different cost structure—you're paying for tonnage, control systems, and safety features, not consumable wear parts. The same TCO spreadsheet logic applies, but the variables are different. You can't manage both categories with the same template.
I learned this the hard way when I tried to apply my tooling TCO model to a press brake upgrade. The numbers didn't map. Consumable cost per part meant nothing. What mattered was cycle time per bend and setup time between jobs. Different category, different math.
What I Actually Do Now
Our procurement policy now requires three things before any cutting tool purchase above $2,000:
- Cost-per-part calculation using our actual cycle times, not the vendor's demo video.
- A documented trial run on the specific material and machine where the tool will live.
- A scrap-rate check after 100 pieces, not just a visual inspection of the first part.
Is this more work? Yes. Does it slow down purchasing? Somewhat. But over the past 18 months, it's saved us roughly $41,000 in avoidable tooling costs—about 12% of our annual budget—and more importantly, it's kept me from having the same conversation with my operations manager twice.
When This Doesn't Apply
I should be honest about the limits here. If you're a job shop running one-off parts with no repeat work, you can't calculate cost-per-part with any confidence. Buy the mid-tier tool, check the first part, move on. The TCO math needs volume to work.
Same goes for shops where the bottleneck isn't the cutting tool—if your machine is waiting on material or operators half the day, tool life differences get buried in bigger delays. Fix the bottleneck first. Optimize the cutting tool when the spindle is actually the constraint.
And if you're considering additive manufacturing suppliers for a part that currently requires complex tooling, run that comparison separately. Additive changes the cost structure entirely—no tooling wear, different material properties, different lead times. Don't try to fit it into your cutting tool spreadsheet. Why do you press the brake to start a car? You don't—unless the car is designed that way. Same principle. Different categories need different decision frameworks.
Bottom line: the cheapest quote is a data point, not a decision. The number that matters is what you pay per good part, after tool changes, scrap, and the operator time you'll never get back. Track that number for six months and the quote sheet starts telling the truth.